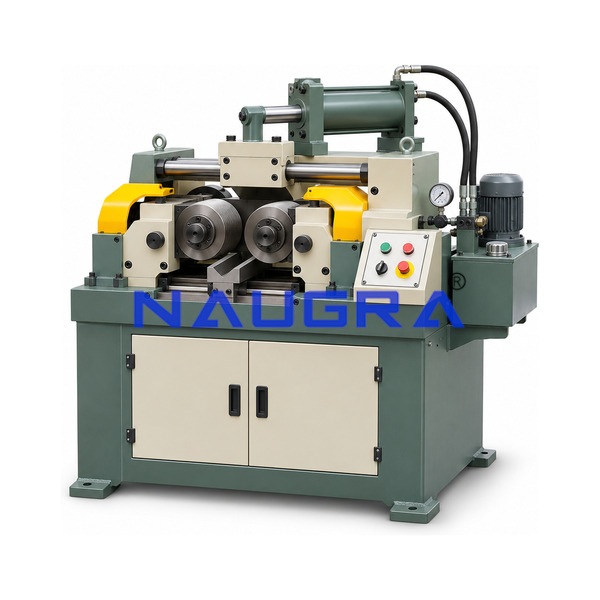
Hydraulic Thread And Form Rolling
Product code: Hydraulic Thread0001Buy Hydraulic Thread And Form Rolling from India
Hydraulic Thread And Form Rolling
Fastener makers and production trainers looking for hydraulic thread and form rolling manufacturers in India need to match workpiece diameter and thread pitch to machine tonnage. Civil Mechanical India is one of the suppliers in India that lists machines of 6 and 12 tonne and workpiece ranges from 3 to 80 mm.
Thread rolling displaces metal instead of cutting it. A blank is pressed between dies, so the thread form is raised from the core, the grain flows with the profile and the thread is stronger and smoother than a cut thread. The main machine in this range takes work of 3 to 24, 3 to 50 and 10 to 80 mm with a thread pitch up to 3, 5 and 10 mm.
The 6 tonne machine suits rods and bolts, and the 12 tonne machine takes larger studs. The flat die machine, with a moving and a fixed die, is used for high volume small screws. Form rolling machines make splines and knurls on shafts and rolled grooves and beads on pipe ends for grooved joints.
Last updated: November 2026
Hydraulic Thread And Form Rolling
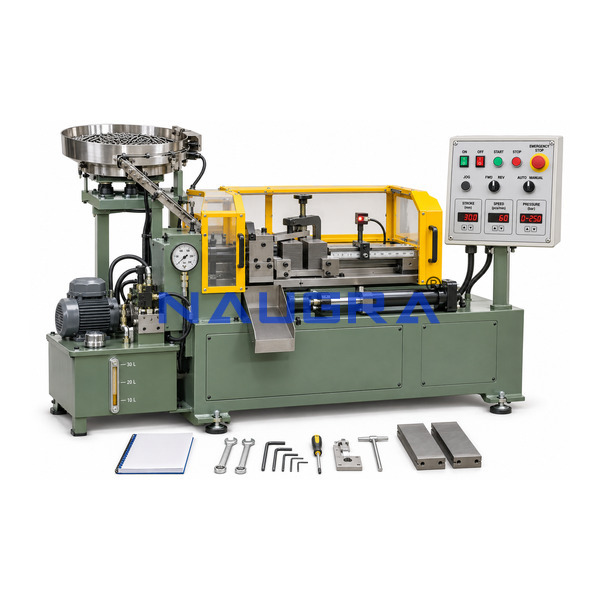
Machine using a moving and fixed flat die to roll threads on small screws and bolts. Used for high volume screw production training. Main ratings: capacity M3 to M10, stroke 300 mm, motor 3 HP, 415 V AC.
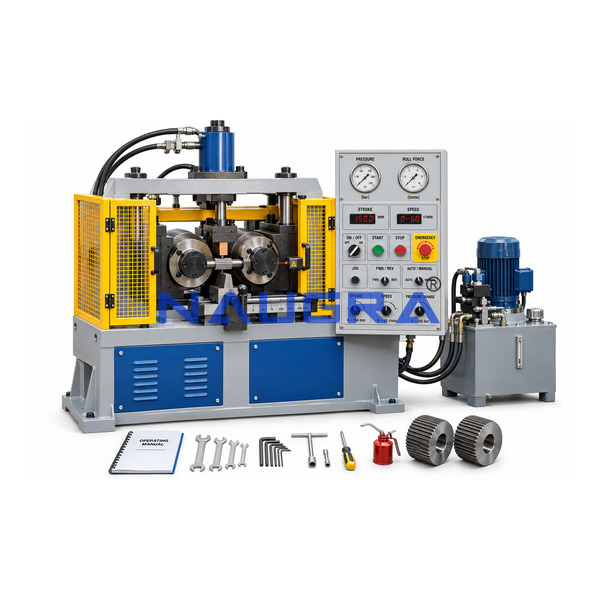
Machine for forming splines and knurls on shafts by rolling. Used in demonstrations of form rolling processes. Main ratings: max diameter 40 mm, roll force 10 tonne, motor 5 HP, 415 V AC.
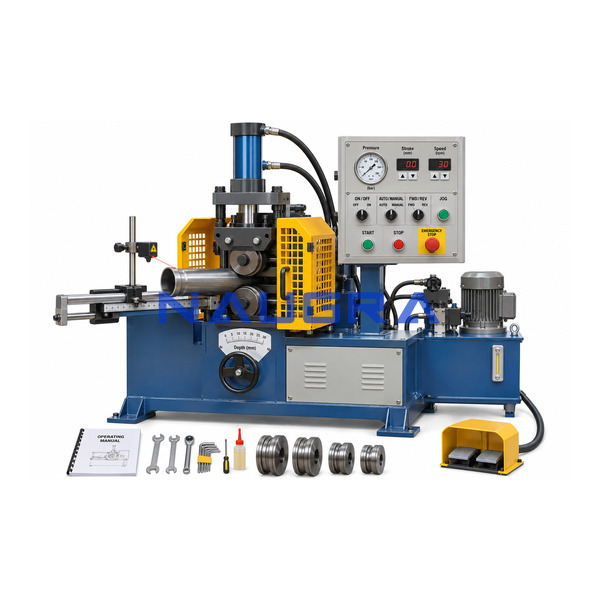
Machine that rolls grooves and beads on pipe ends. Used in plumbing and HVAC training for grooved joints. Main ratings: pipe size 1 to 4 inch, motor 2 HP, 415 V AC, roll Grooving.
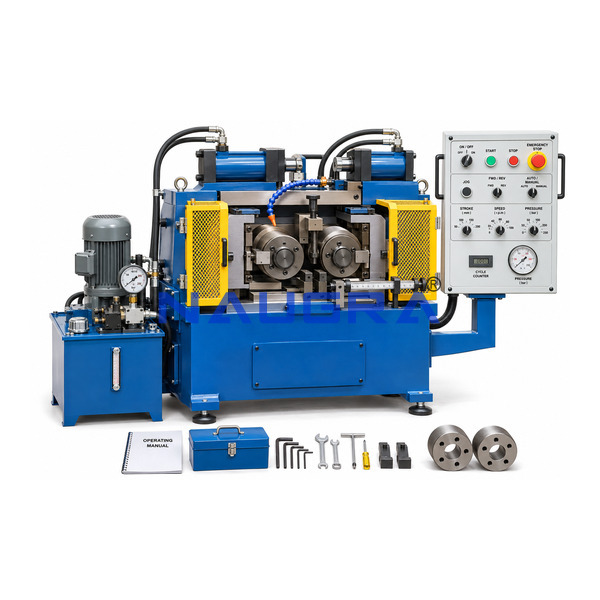
Heavier thread rolling machine for larger diameter bolts and studs. Used in labs to demonstrate rolled thread production on bigger sizes. Main ratings: capacity M10 to M20, roll force 12 tonne, motor 5 HP, 415 V AC.
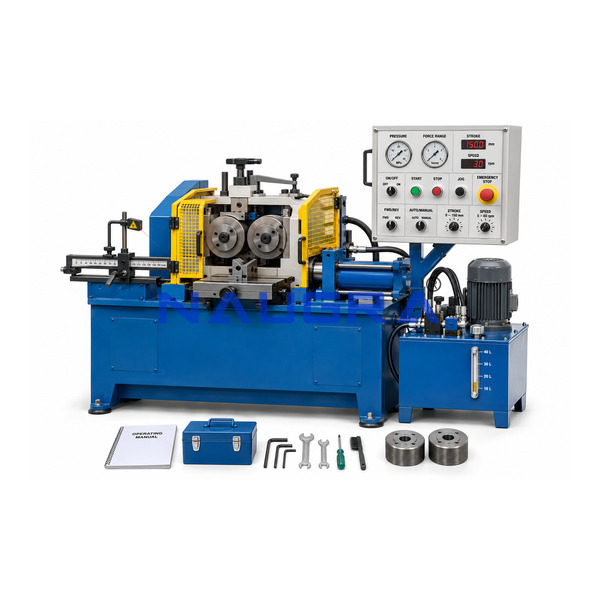
Hydraulic machine that forms external threads on bolts and rods by rolling between flat or round dies. Used in production training to show cold forming of threads without cutting.
| Function | Products | What to confirm |
|---|---|---|
| Thread rolling | Hydraulic Thread Rolling Machine 6 Tonne, Hydraulic Thread Rolling Machine 12 Tonne, Hydraulic Thread And Form Rolling | Workpiece diameter, maximum pitch, rolling force and die set size |
| Flat die rolling | Hydraulic Flat Die Thread Rolling Machine | Screw diameter range, die length, output per minute and blank feeding method |
| Form and end rolling | Hydraulic Form Rolling Machine For Splines, Hydraulic Pipe End Form Rolling Machine | Spline or groove profile, pipe diameter range, die tooling and cycle length |
A hex nipple machine cuts threads with a die head, removing metal as chips. A thread rolling machine does not cut anything. It cold forms the thread by pressing, which gives stronger threads and no chips, but it needs a blank turned to the pitch diameter. Choose rolling for bolts and studs in volume and cutting for pipe nipples.
See also: Hex Nipple Threading Machine Suppliers
The complete Hydraulic Thread And Form Rolling range (6 products), in alphabetical order:
Choose by the largest thread diameter and pitch, and the material. Higher strength steel needs more force. Give us the diameter, pitch and steel grade, and we check against 6 or 12 tonne ratings. Die set sizes should be listed one per thread size.
The blank diameter should be close to the pitch diameter of the thread, which is smaller than the major diameter. Poor blank size results in incomplete thread or die damage. Ask for guidance on blank sizes for your thread standard.
A lab needs a clear guard, pressure gauge, die setting jig and a roller inspection routine. Demonstrating rolled versus cut threads with a section microscope is a useful classroom exercise. Check also that the die setting is shown with a simple jig, so students can learn to align the two dies parallel before each run.
Typical buyers are bolt and screw manufacturers, forging and fastener units, pipe and HVAC fabricators for grooved ends, and technical colleges teaching metal forming. Vocational centres also buy form rolling machines to demonstrate spline and knurl production. Rolled studs and screws are also needed by anchor and fastener makers, who buy these presses with die sets for a particular thread series.
The grain flows along the thread profile and the surface is work hardened. A cut thread severs the grain, so fatigue strength is lower. This also gives smoother thread flanks, and the rolled core is stronger in tension, which is why high strength bolts are rolled.
Yes, dies are made for a particular thread form and pitch. Order die sets with the machine. A die set made for a metric 1.5 mm pitch cannot roll a 2 mm pitch, so spare sets should be priced with the machine at the start.
It rolls grooves and beads on pipe ends, used in grooved coupling joints in plumbing and HVAC. The same machine can be used to put beads and grooves on pipe ends that take quick couplers or clamps in pipelines and ducts.
Yes, a lubricating coolant reduces die wear and gives a smooth surface. The oil also carries away heat and fine particles from the die faces, and should be filtered and replaced at the interval stated in the manual.
Yes, please share the destination, voltage and tooling needs. These presses are heavy, so crate weight is stated in advance, and spare die sets can be packed in the same shipment.
As established manufacturers and suppliers for tender requirements from India, we undertake civil laboratory and industrial testing tenders as well as bulk and OEM supply of mechanical engineering and testing laboratory equipment. Please forward your tender specifications and our team will prepare a detailed quotation for Hydraulic Thread And Form Rolling.
Send us your equipment list or tender specification. We quote against IS, BS, EN, ASTM and AASHTO standards and ship to 90+ countries.